OKOndt Group
OKOSCAN 73HS High-Speed Ultrasonic and Eddy Current Rail Testing System
Manufacturer product description
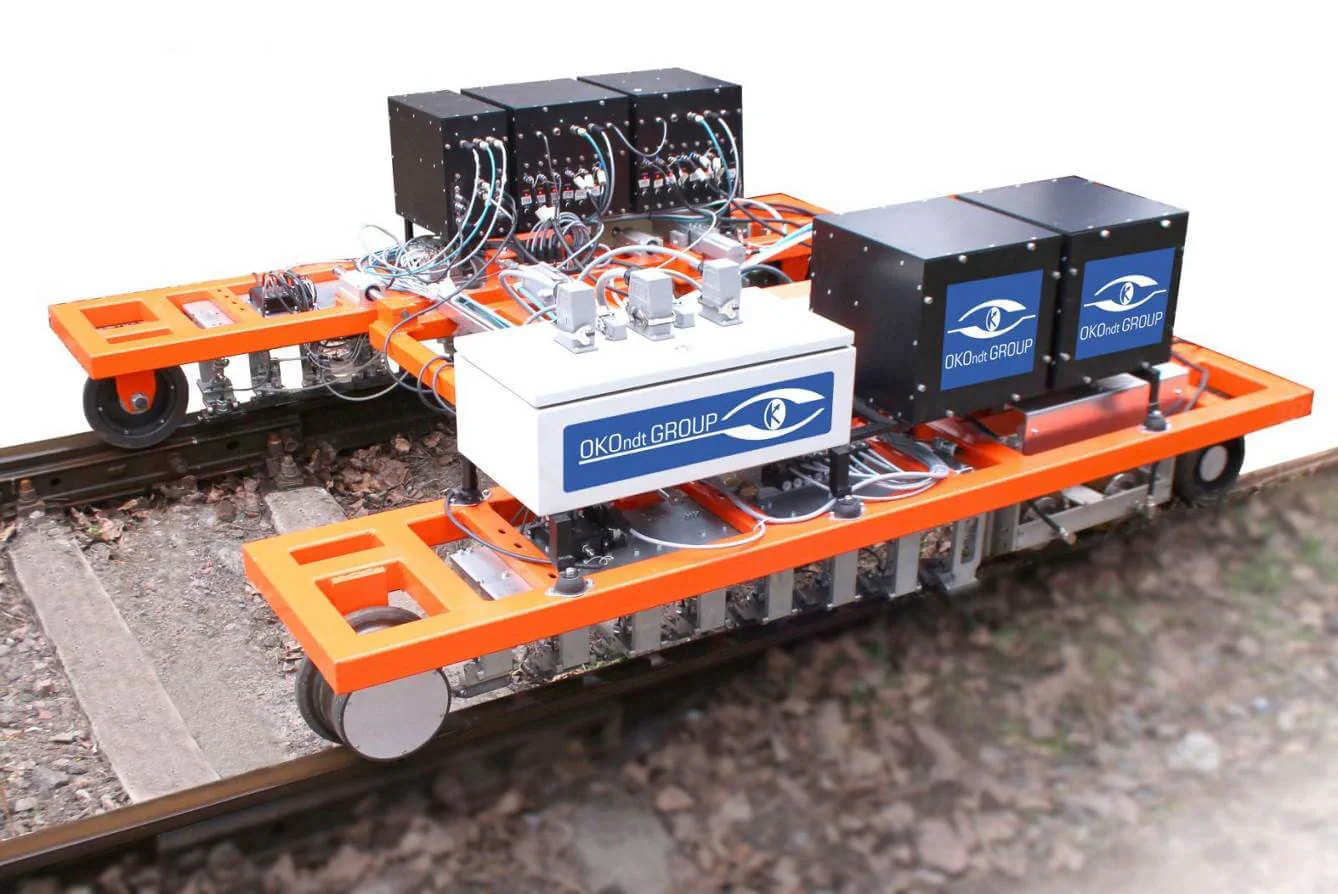
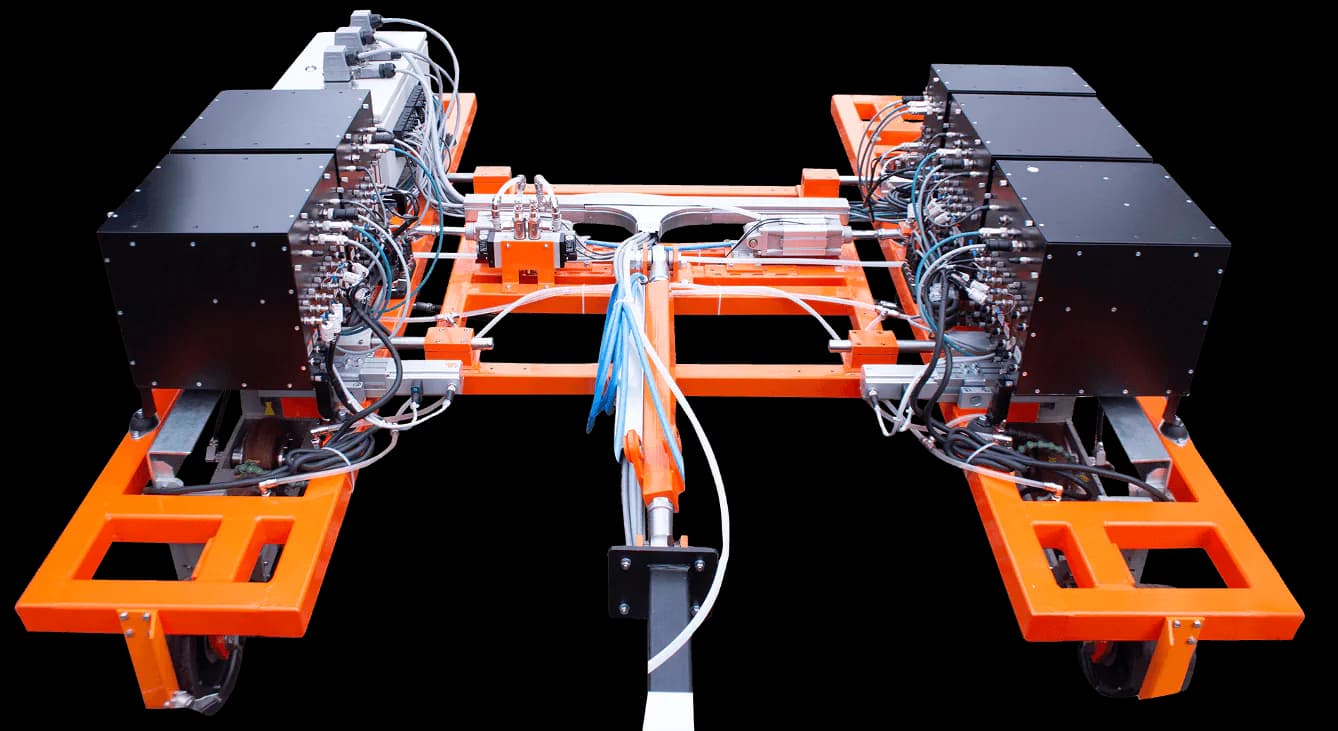
The OKOSCAN 73HS System is intended for automated high-speed testing of rail in service
OKOSCAN 73HS High-Speed Ultrasonic and Eddy Current Rail Testing System
5 more images are not shown on this page.
- Brand
- OKOndt Group
- Category
- Eddy current testing
- Method / product family
- Model
- OKOSCAN 73 HS
Technical Specifications
| Product model | OKOSCAN 73 HS |
|---|---|
| Flaw detector type | Double rail |
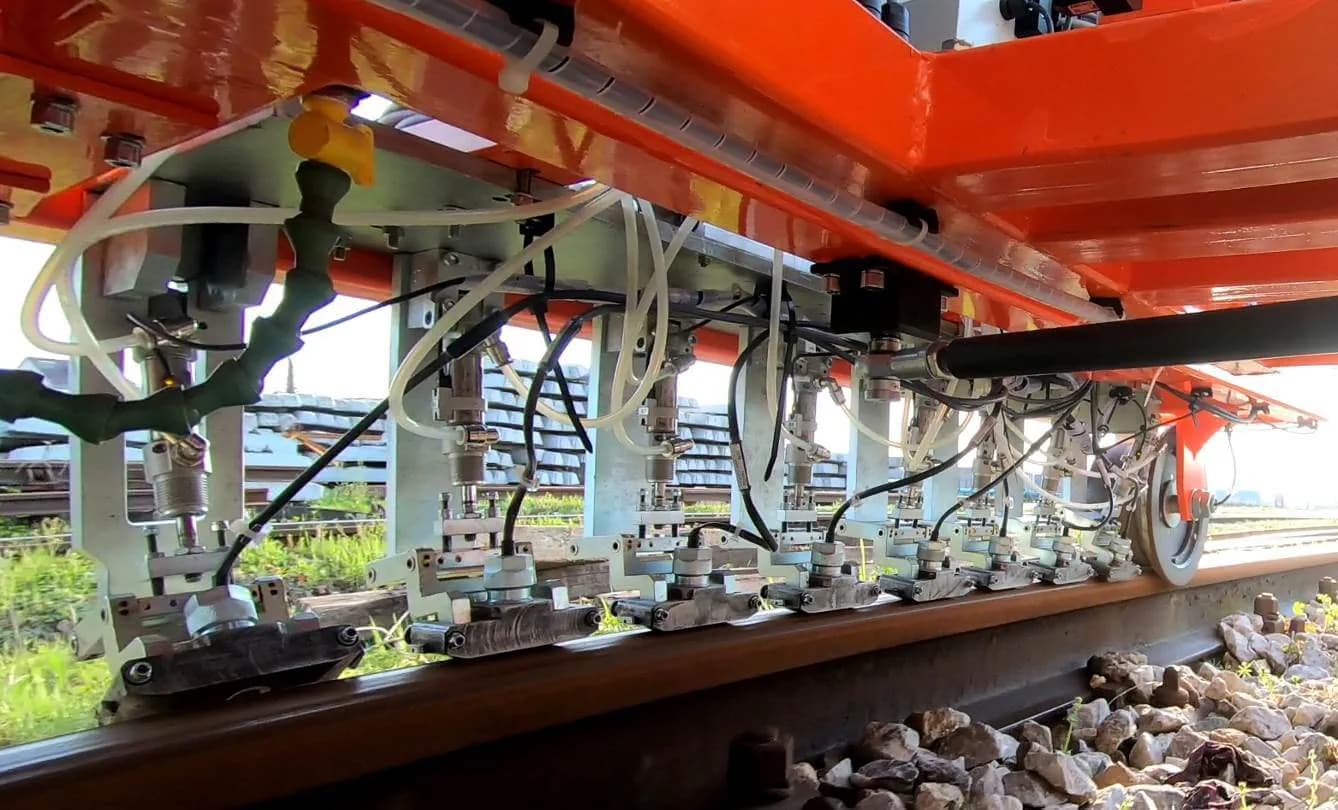
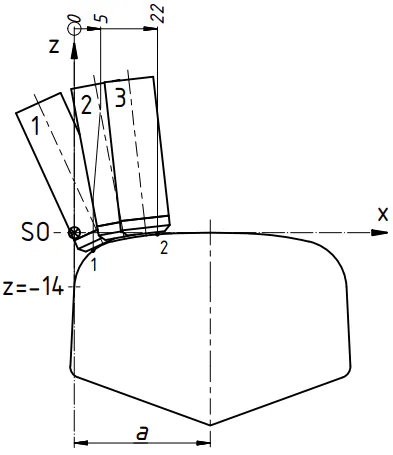
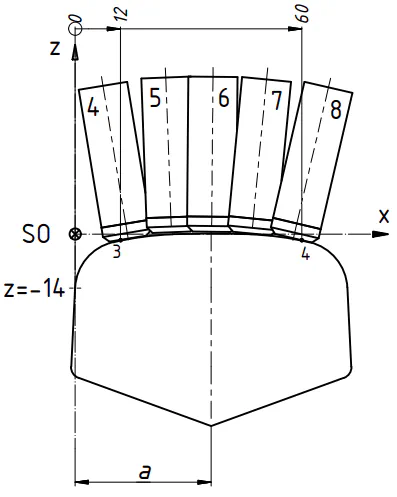
| Areas of testing | Rail gauge corner Rail running surface |
| Quantity of EC Ps of the flaw detector | 16 |
| Quantity of EC Ps per rail | 8 |
| Area of coverage of the probe | 6 mm |
| Probe operating frequency | 200 kHz |
| ECP protection from mechanical damage and wear | Ceramic protector |
| Testing speed | Up to 40 km/h |
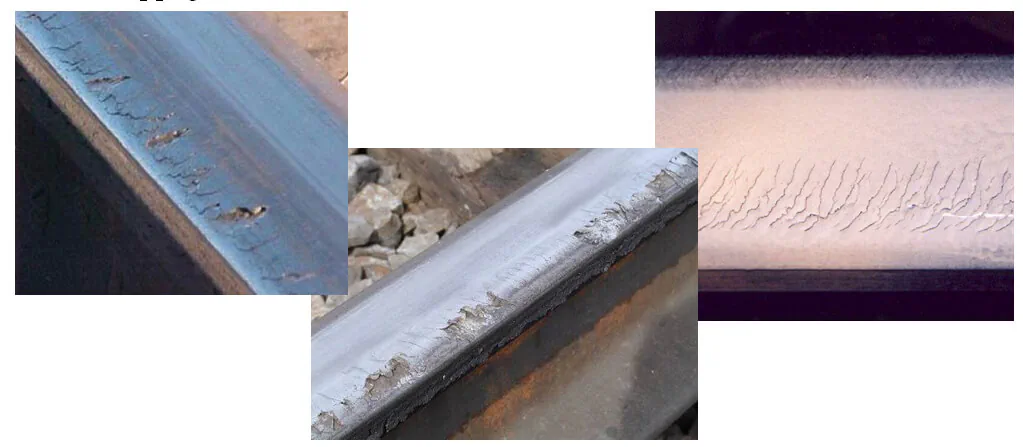
| Assessment of the cracks vertical component depth (for 25⁰ angle of the crack progression) | From 0.7 mm to 3.4 mm |
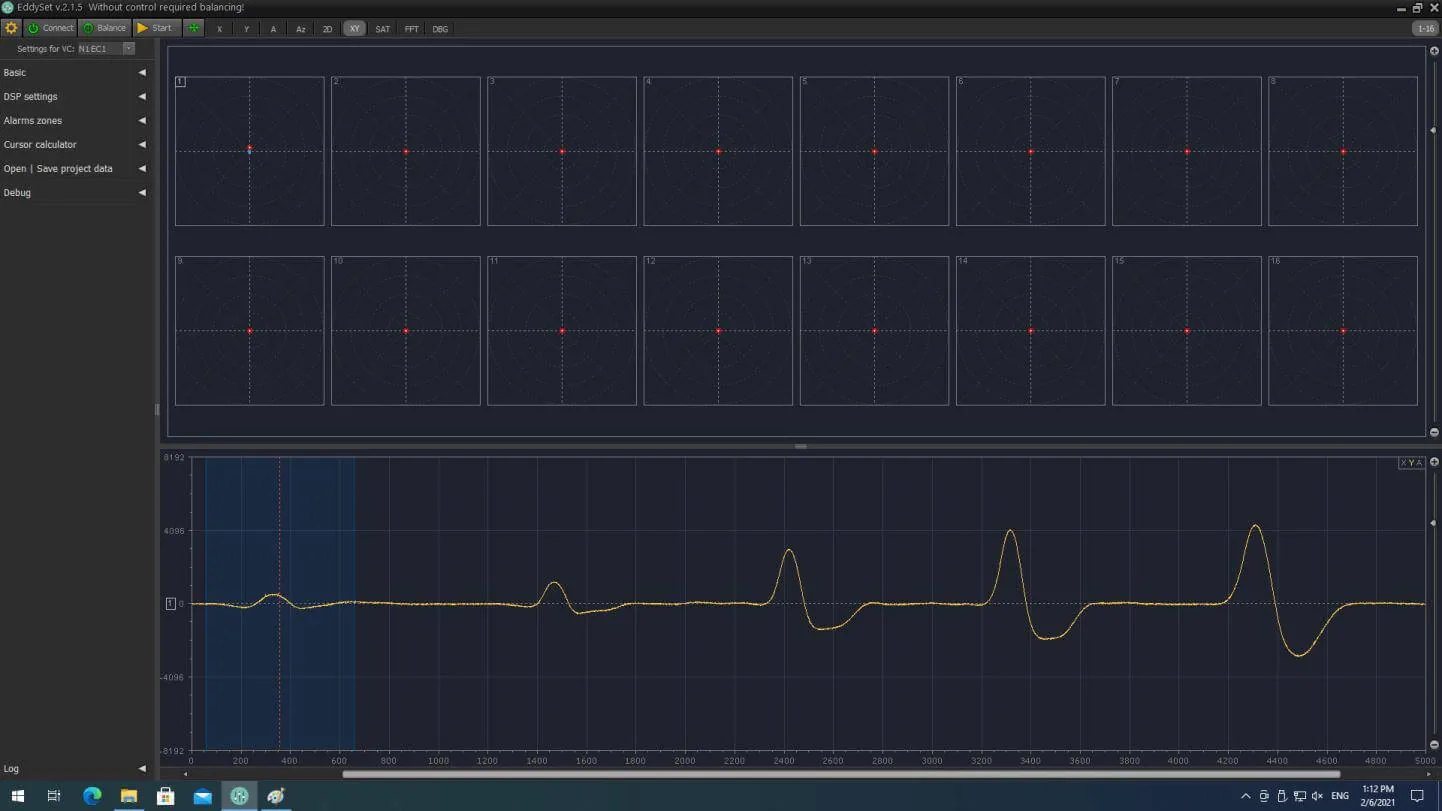
| Eddy current channel | Eddycon D |
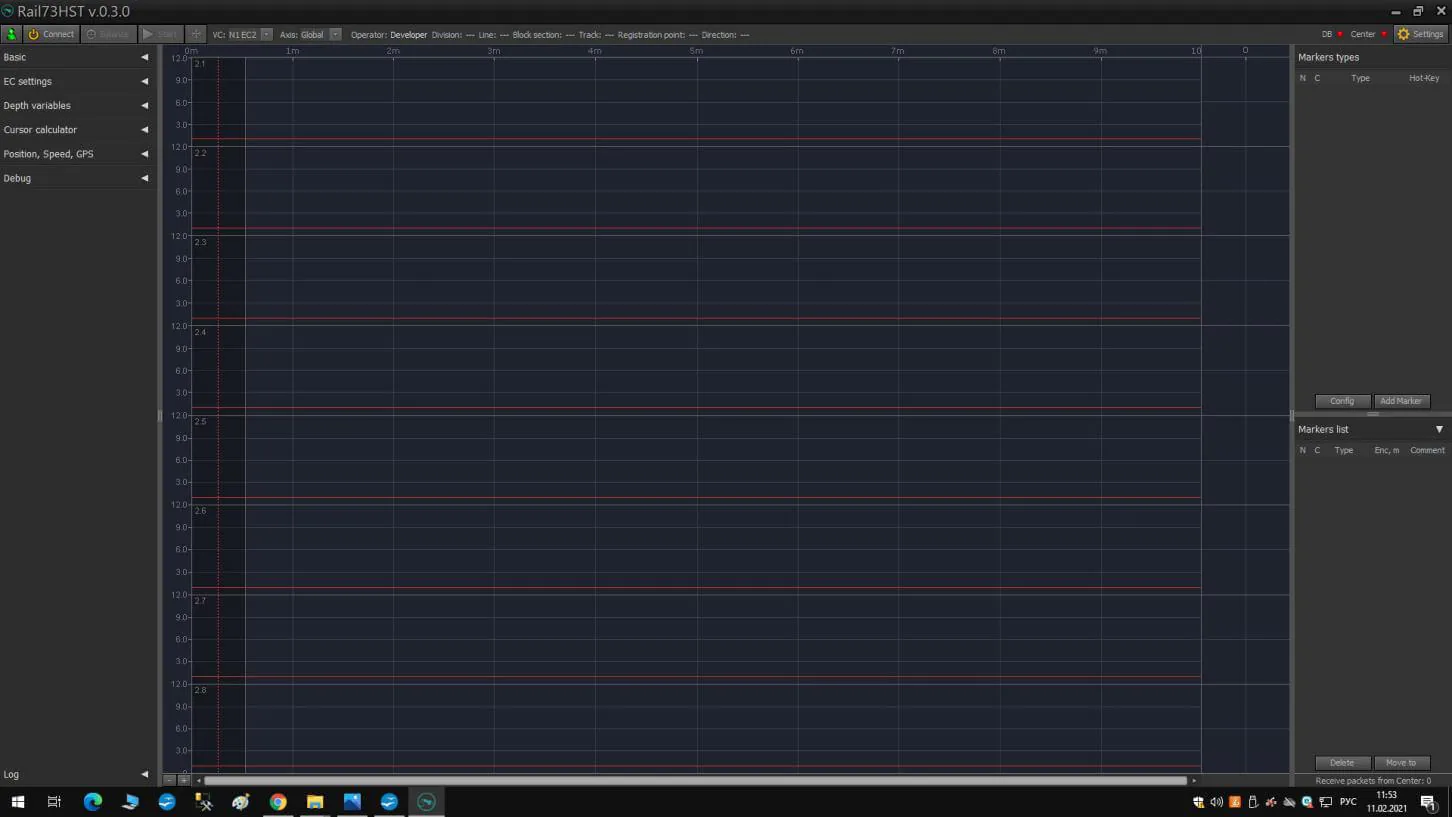
| Specialized software | - Setting program - Testing program - Results viewing program |
| Data record and storage | PC’s hard drive |
| Operating PC | Laptop – for setting and testing programs Desktop – for results viewing program |
| Parameters of tested areas and of the flaws detection efficiency — 1 | Name: Close dead area | Value: Crystal probe 0° : 8 mm; Crystal probe 40° : 5 mm); Crystal probe 70° : 3 mm; Crystal probe (CCP) 55° - 5 mm; ECP - none. |
| Parameters of tested areas and of the flaws detection efficiency — 2 | Name: Tested Area | Value: Ultrasonic testing: Crystal probe 0° : full rail height; Crystal probe 40° : full rail height; Crystal probe 70° : rail head Crystal probe 55° - rail head; Eddy Current Inspection: 5 ECP - rail running surface; 3 ECP - rail working edge; |
| Parameters of tested areas and of the flaws detection efficiency — 3 | Name: Resolution with references to the coordinates - Longitudinal coordinate - Depth - Rail height; | Value: 1.0 mm; 0.1 mm; 0.1 mm |
| Parameters of tested areas and of the flaws detection efficiency — 4 | Name: Assessment of the cracks vertical component depth by eddy- current method | Value: from 0.7 mm to 3 mm |
| Parameters of tested areas and of the flaws detection efficiency — 5 | Name: Accuracy of determining the parameters during ultrasonic testing: - Depth - Rail height; | Value: ± 0.5 mm ± 0.5 mm |
| Parameters of tested areas and of the flaws detection efficiency — 6 | Name: GPS | Value: Recording the global positioning coordinate in the control file and then viewing it on a computer |
| Parameters of tested areas and of the flaws detection efficiency — 7 | Name: Minimally detectable defects | Value: Ultrasonic testing (at a 2 mm sonic test pitch) Cylindrical hole of 2 mm diameter in the rail head 5 mm deep and 1.5 mm wide groove in the working edge of the rail head (or 5 mm diameter flat bottom hole in the working edge), transverse crack simulation. 5 mm deep, 2 mm wide groove in the rail base, corrosion simulation Eddy Current Inspection: 1.2 mm deep “cut” is made on the running surface in the sectional plane |
Technical specifications are taken from data published by the supplier; refer to the supplier source for final and binding values.
Product Documents
Request a product quote
Add the NDT and PWHT equipment, consumables and spare parts you wish to purchase to your product quote list.